

Regular price
$149.99
Sale price
$149.99
Regular price
Unit price
per
Low Stock
We Accept
Product details
Features & specifications
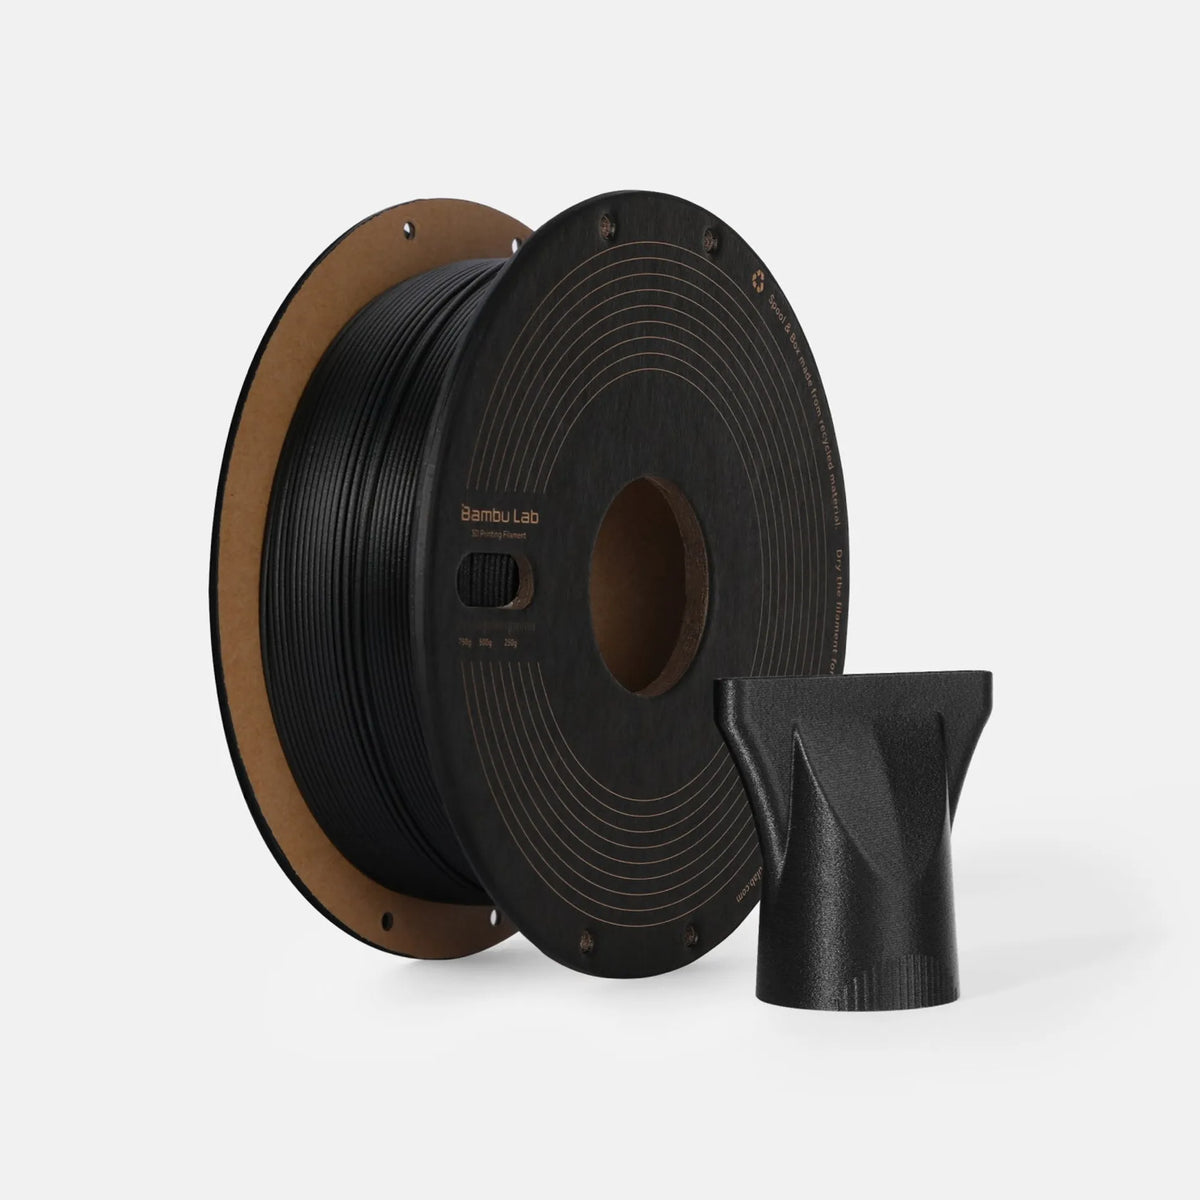
Bambu Lab PPA-CF is a 1.75mm carbon fiber reinforced PPA filament with strength approaching metal levels: 48% stronger and 102% stiffer than normal PA6-CF. It stays stable in humid conditions and at high temperatures, which makes it a fit for high-performance engineering parts, repairs, and industrial or automotive components. It needs a hardened steel nozzle.
Highlights
- Metal-like strength. 208 MPa bending strength and 9860 MPa stiffness in the dry state.
- Industrial-grade precision. Superior dimensional stability, without warping or deformation.
- Stable in humid conditions. Moisture absorption 66% lower than normal PA6-CF, for long-term use in humid environments, even underwater.
- Unmatched heat performance. A heat deflection temperature of 227°C at 0.45 MPa.
Mechanical Properties
| Property | PPA-CF | Bambu PA6-CF | Standard PA6-CF |
|---|---|---|---|
| Bending modulus (XY, dry) | 9860 MPa | 5460 MPa | 4870 MPa |
| Bending modulus (XY, wet) | 9620 MPa | 3560 MPa | 1890 MPa |
| Stiffness decline when wet | 2.4% | 34.8% | 61.2% |
| Bending strength (XY, dry) | 208 MPa | 151 MPa | 141 MPa |
| Bending strength (XY, wet) | 202 MPa | 95 MPa | 67 MPa |
| Strength decline when wet | 2.9% | 37.1% | 52.5% |
| Saturated water absorption (25°C, 55% RH) | 1.30% | 2.35% | 3.80% |
Specifications
| Material | PPA with carbon fiber |
| Diameter | 1.75mm ± 0.05mm |
| Net weight | 0.75 kg per roll |
| Format | With spool |
| AMS | Not compatible with any AMS series |
| Nozzles | Hardened steel nozzle mandatory. The 0.2mm nozzle is not compatible |
| Accessories | Not compatible with the Cool Plate SuperTack or Bambu Liquid Glue |
Printing and Care
- Must be dried. Dry before use for the best print quality. Higher temperatures within the drying range work better, but do not exceed 160°C to avoid damaging the spool.
- Store it airtight. Use an airtight container with desiccant during printing so the filament does not absorb moisture.
- Coat the plate. A thin coat of glue stick prevents the filament from damaging the print surface and helps the model adhere.
- Orient for the load. Print performance depends on orientation, wall loops, infill pattern and density, size, and shape. The XY direction is significantly stronger than Z.
- Wear gloves. Carbon fiber filament can produce fine fiber debris, and the filament surface and ends may carry hard microscopic splinters. Wear puncture- and cut-resistant gloves and safety goggles when loading filament, removing supports, cutting, or sanding, and avoid touching rough edges and cross-sections with bare hands.
- Print safely. Use a well-ventilated area, and keep filament and fragments away from children and pets. This filament is not food-grade, so do not use finished prints for food storage or contact.